Heavy equipment is the operational backbone of modern industry. From mining sites and construction zones to manufacturing plants and logistics hubs, these machines convert raw effort into precise, repeatable output at a scale no workforce could achieve alone. For decision-makers evaluating capital investment, operational efficiency, or safety strategy, understanding the true scope of heavy equipment’s role is essential. This article examines how heavy machinery drives productivity, shapes cost structures, and influences the strategic direction of industrial operations.
Defining Heavy Equipment in the Industrial Context
Heavy equipment refers to the high-capacity machines engineered for demanding physical work: excavation, lifting, hauling, compaction, drilling, and material processing. Unlike general-purpose tools, these assets are purpose-built for durability, load capacity, and continuous duty cycles in harsh environments.
Common categories include:
- Earthmoving equipment — excavators, bulldozers, loaders, and backhoes
- Lifting and handling machinery — cranes, telehandlers, and forklifts
- Hauling and transport assets — dump trucks, articulated haulers, and conveyors
- Processing equipment — crushers, screeners, and concrete mixers
- Specialized industrial machinery — drilling rigs, pipelayers, and compaction units
Each category carries distinct operational characteristics, maintenance requirements, and total cost of ownership profiles — factors that directly affect industrial planning.
Productivity and Throughput: The Core Value Proposition
The primary role of heavy equipment is to multiply output per labor hour. A single hydraulic excavator can move hundreds of cubic meters of material per shift, work that would otherwise require a large manual crew over several days. This multiplier effect is particularly significant in industries where throughput determines profitability.
Beyond raw capacity, modern heavy equipment contributes to productivity through:
The result is a measurable lift in output, schedule certainty, and cost efficiency across the entire operation.
Safety and Risk Management
Heavy equipment plays a dual role in safety: it introduces significant hazards if mismanaged, yet it also removes workers from the most dangerous tasks. Well-run industrial operations treat equipment safety as a core discipline, not a compliance formality.
Key safety contributions of properly deployed heavy machinery include:
- Replacing manual handling of heavy loads, reducing musculoskeletal injuries
- Enabling remote and autonomous operation in high-risk zones
- Providing operator-assist technologies such as collision detection and load monitoring
- Supporting structured inspection and maintenance regimes that prevent failures
Organizations that invest in operator training, machine guarding, and preventive maintenance consistently report lower incident rates and reduced downtime — a direct link between equipment management and operational resilience.
Economic Impact: Cost Structures and Total Ownership
Heavy equipment represents one of the largest capital expenditures in industrial operations. Understanding its economic role requires looking beyond purchase price to the total cost of ownership, which includes fuel, maintenance, operator labor, insurance, and depreciation.
| Depreciation / Acquisition | 25–35% | Fleet right-sizing, residual value planning |
| Fuel and Energy | 20–30% | Machine selection, idle-time reduction |
| Maintenance and Repair | 15–25% | Preventive maintenance, telematics data |
| Operator Labor | 10–20% | Training, automation, ergonomics |
Strategic decisions — buy versus lease, new versus refurbished, owned fleet versus contracted services — depend on accurate modeling of these cost drivers. Heavy equipment is therefore not merely an operational asset but a financial one that shapes balance sheets and cash flow.
Technology and the Modern Equipment Lifecycle
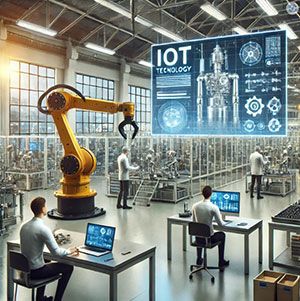
Digital transformation has fundamentally changed what heavy equipment contributes to industrial operations. Telematics systems stream data on machine health, fuel consumption, location, and operator behavior. Predictive maintenance algorithms flag component wear before failure occurs. Autonomous haulage and semi-automated earthmoving are moving from pilot programs into mainstream deployment.
These technologies shift the emphasis from reactive repair to proactive asset management. Operations that leverage equipment data effectively gain advantages in uptime, safety, and cost control — and they build the analytical foundation for further automation.
Sustainability and Regulatory Pressures
Emissions regulations, noise limits, and site sustainability targets increasingly shape equipment strategy. Electrification of compact and mid-size machines, hybrid drivetrains, and alternative fuels are gaining traction, particularly in urban construction and enclosed industrial environments. Fleet managers must plan for transition costs while maintaining productivity — a balancing act that positions heavy equipment squarely within environmental, social, and governance (ESG) strategy.
Conclusion
Heavy equipment is far more than a fleet of machines; it is a strategic enabler of industrial performance. It determines throughput, anchors safety outcomes, dominates capital and operating cost structures, and increasingly serves as a data source for intelligent operations. Organizations that treat equipment as a managed, measured, and continuously optimized asset — rather than a fixed cost — position themselves to compete on productivity, resilience, and sustainability. The role of heavy equipment in industrial operations is, in short, foundational: get it right, and the rest of the operation follows.